How to Evaluate the QC Capabilities of an Overseas Sheet Metal Fabricator: A Buyer's Checklist
Overseas sheet metal fabrication offers compelling cost advantages, but the quality risks are real and expensive. A single batch of out-of-tolerance brackets, a falsified material certificate, or a coating that fails adhesion testing can cascade into production line shutdowns, warranty claims, and damaged customer relationships. The difference between a smooth overseas sourcing program and a costly failure often comes down to one thing: how thoroughly you evaluate a supplier's Quality Control (QC) and Quality Assurance (QA) capabilities before placing that first production order.
This guide breaks down the critical pillars of sheet metal quality control — Certifications, Material Traceability, Inspection Equipment, Inspection Documentation, Supplier Qualification, Cost Evaluation, Lead Time Assessment, Communication & Cultural Management, Risk Management, and New Product Introduction — into a practical, actionable checklist you can use during supplier audits. Each section includes the specific questions to ask, the documents to request, and the red flags that separate a reliable manufacturing partner from a risky one.
The Sourcing Dilemma: Why QC Evaluation Matters More Than Price
Overseas sheet metal manufacturing offers huge cost savings, but quality inconsistency, material fraud, and out-of-tolerance parts can ruin supply chains. Cost savings on paper mean nothing if your parts fail incoming inspection, if your assembly line goes down because a supplier shipped non-conforming components, or if your end customer discovers corrosion failure in the field six months after installation.
The solution is a structured, evidence-based audit of a supplier's QC and QA capabilities before placing production orders. This is not about distrust — it's about verification. A supplier with genuine quality systems will welcome the scrutiny, because it demonstrates that you understand manufacturing and that you're serious about a long-term partnership.
What this guide covers: the complete framework for evaluating overseas sheet metal suppliers — from certifications and material traceability to cost negotiation, lead time assessment, communication management, risk mitigation, and new product introduction. Each section provides concrete questions, verification methods, and red flag alerts.
Pillar 1: Certifications & Management Systems (ISO 9001 & Beyond)
Why ISO 9001:2015 Matters — And What It Doesn't Guarantee
ISO 9001:2015 is the most widely recognized quality management standard in sheet metal fabrication. It signals that a supplier has documented processes for order review, production control, inspection, corrective action, and continual improvement. It does not guarantee perfect parts — it guarantees that the supplier has a system to catch and correct problems.
However, a certificate alone proves very little. Many shops claim ISO 9001 compliance but have never been audited by an accredited registrar. Always request the certificate and verify the registrar's accreditation through the issuing body's official database. Check the certificate's scope, expiry date, and the specific legal entity it covers.
Audit questions:
-
Can you provide the ISO 9001:2015 certificate with the registrar's accreditation number?
-
Who is the certification body, and when was the last surveillance audit?
-
Can we review your internal audit records and corrective action logs from the past 12 months?
Red flag alert: Supplying fake certificates or lacking verifiable audit numbers is a serious integrity issue. One documented case involved a medical device assembly line going down three weeks into production when the procurement team discovered the ISO 9001 certificate attached to their new Chinese supplier's quote was a copy issued to a completely different company — one that had never produced a single sheet metal component.
Industry-Specific Certifications to Look For
| Certification | Industry Focus | What It Adds Over ISO 9001 |
|---|---|---|
| IATF 16949 | Automotive | PPAP requirements, advanced product quality planning, statistical process control |
| ISO 13485:2016 | Medical Devices | Design controls, biocompatibility traceability, regulatory compliance |
| AS9100D | Aerospace & Defense | Configuration management, risk management, FOD prevention |
| ISO 14001 | All (Environmental) | Environmental impact management, waste reduction |
If your supplier claims IATF 16949 for automotive sheet metal components, ask to see a recent PPAP package. If they claim ISO 13485 for medical enclosures, verify their cleanroom classification and biocompatibility test reports.
Key takeaway: Verify every certification against the issuing body's database, and request the audit report — not just the certificate.

Pillar 2: Material Traceability & Material Test Certificates (MTC / Mill Test Report)
The Risk of Substandard Metals
The wrong material grade can cause catastrophic failures. Impurities in stainless steel lead to intergranular corrosion. Lower aluminum grades crack during bending. Uneven sheet thickness creates assembly fit issues and weakens structural joints.
What Is an MTC (EN 10204 3.1)?
An EN 10204 3.1 Mill Test Certificate is an inspection document issued by the material manufacturer's independent inspection department. It includes actual test data from the specific heat of material delivered — not generic specification values. The certificate verifies chemical composition and mechanical properties including tensile strength, yield strength, and hardness.
The Critical Check Most Buyers Miss
The single most dangerous traceability gap occurs when the heat number stamped on the steel doesn't match the heat number on the certificate you've been given. The batch that arrived isn't the batch that was tested.
Before fabrication starts, verify three things:
-
The heat number stamped on the raw material matches the certificate
-
The mechanical property values meet the structural specification
-
The certificate type (EN 10204 3.1 or higher) matches your project requirements
RFQ language to embed in your purchase documents:
| RFQ Line Item | Example Language |
|---|---|
| Material Specification | “Material shall be [grade] with full MTR per EN 10204 3.1.” |
| Heat Number Requirement | “Heat number must be marked on all raw material and traceable to the MTR.” |
| Documentation Delivery | “MTRs and Certificates of Conformance (CoC) shall be delivered with or before shipment.” |
| Retention Requirement | “Supplier shall retain copies of all MTRs for a minimum of 10 years.” |
| Non-Compliance Clause | “Material received without valid MTR documentation will be rejected.” |
Ask during the quoting phase. If you wait until after delivery, it is often too late. Once the material leaves the mill and enters a fabricator's inventory, the link between the physical metal and its documentation can break.
Key takeaway: Embed traceability requirements in your RFQ before quoting begins. Verify heat number match on every incoming shipment.
Pillar 3: Inspection Equipment & Measurement Capabilities
Basic Gauges vs. Precision Metrology
The inspection equipment a supplier owns reveals their true quality capability. During a factory audit, verify that the equipment is not only present but operational — check calibration stickers for current dates.
Basic inspection tools you should see:
-
Digital calipers and micrometers (verify calibration status)
-
Height gauges and depth gauges
-
Pin gauges and thread gauges for hole verification
-
Bend angle measurement devices for press brake verification
Advanced CMM (Coordinate Measuring Machine) Inspection
For parts with tight-tolerance features, complex hole patterns, or 3D positional tolerances, CMM inspection is mandatory. CMM capability is particularly critical for verifying:
-
Positional tolerances of hole patterns across multi-bend components
-
Complex form and flatness requirements
-
Tight-tolerance press brake bends
-
GD&T callouts that cannot be verified with hand tools
Key takeaway: Verify equipment is operational with current calibration. Require CMM reports for tight-tolerance features.
Surface Quality & Coating Testers
| Test | Standard | Target |
|---|---|---|
| Dry Film Thickness (DFT) | Calibrated magnetic/eddy current gauge | 2–3 mils for most applications |
| Adhesion | ASTM D3359 cross-hatch | No coating lift-off |
| Corrosion Resistance | ISO 9227 Neutral Salt Spray (NSS) | 500–1,000 hours for industrial applications |
For salt spray testing, specify ASTM B117 or ISO 9227 in your procurement documents. A proper salt spray test report should include the testing standard referenced, test duration, solution parameters, and photographic evidence.
Pillar 4: Quality Documentation & Inspection Reports (The Proof of Quality)
First Article Inspection (FAI) — The Single Most Informative Document
The First Article Inspection Report is arguably the most informative document in a supplier's quality system. It shows whether measured values are compared against a stated requirement, whether the measurement method is named row by row, and whether someone signed and dated it. For aerospace applications, FAI must conform to AS9102.
What to require in your FAI request:
-
Current revision-level drawings with ballooned dimensions
-
Material grade and thickness specifications
-
Critical tolerance callouts and GD&T requirements
-
Dimensional inspection data for every ballooned feature
-
Material certifications and process records
In-Process Quality Control (IPQC)
-
First-off inspection during stamping and bending operations
-
Periodic sampling during production runs based on AQL standards
-
Tool wear monitoring for cutting and forming operations — a supplier who tracks tool wear has a system in place; a supplier who doesn't is guessing
-
Bend angle verification after press brake forming
Outgoing Quality Control (OQC) / Final Inspection Report
The final inspection report should include dimensional inspection records, visual defect checks, coating verification, and packing specification compliance. A report that says "checked, OK" without numbers is a description, not a record.
Key takeaway: Require FAI before mass production. Never accept final inspection reports without numerical data.

Pillar 5: Supplier Qualification & Capability Assessment
Before placing any production order, you need to verify that the supplier has the technical capabilities to manufacture your parts to specification. A supplier audit checklist for sheet metal fabrication should evaluate manufacturing capability across cutting, forming, welding, and finishing processes.
In-House vs. Subcontracted Operations
The single most important question to ask during a facility audit: Which operations are done in this building, and which are not?
A supplier that subcontracts laser cutting or powder coating loses direct control over quality, lead time, and corrective action. Every handoff between vendors is a potential quality escape point. When critical processes are outsourced, you lose visibility into whether the subcontractor follows your specifications.
Equipment & Capacity Verification
Questions to ask:
-
How many laser cutters, press brakes, and welding stations do you operate?
-
What is your current capacity utilization rate? (70–85% is ideal — it shows they have buffer capacity without being underutilized)
-
How many shifts do you run? Can you add shifts or temporary skilled labor?
-
Do you use ERP or MRP software for production scheduling?
Green flags: Multiple machines of the same type (equipment redundancy), digital scheduling with real-time tracking, cross-trained operators, documented ramp-up case studies.
Red flags: Single machine for critical processes, manual scheduling on whiteboards, vague answers about past ramp-ups, utilization over 90% with no room for growth.
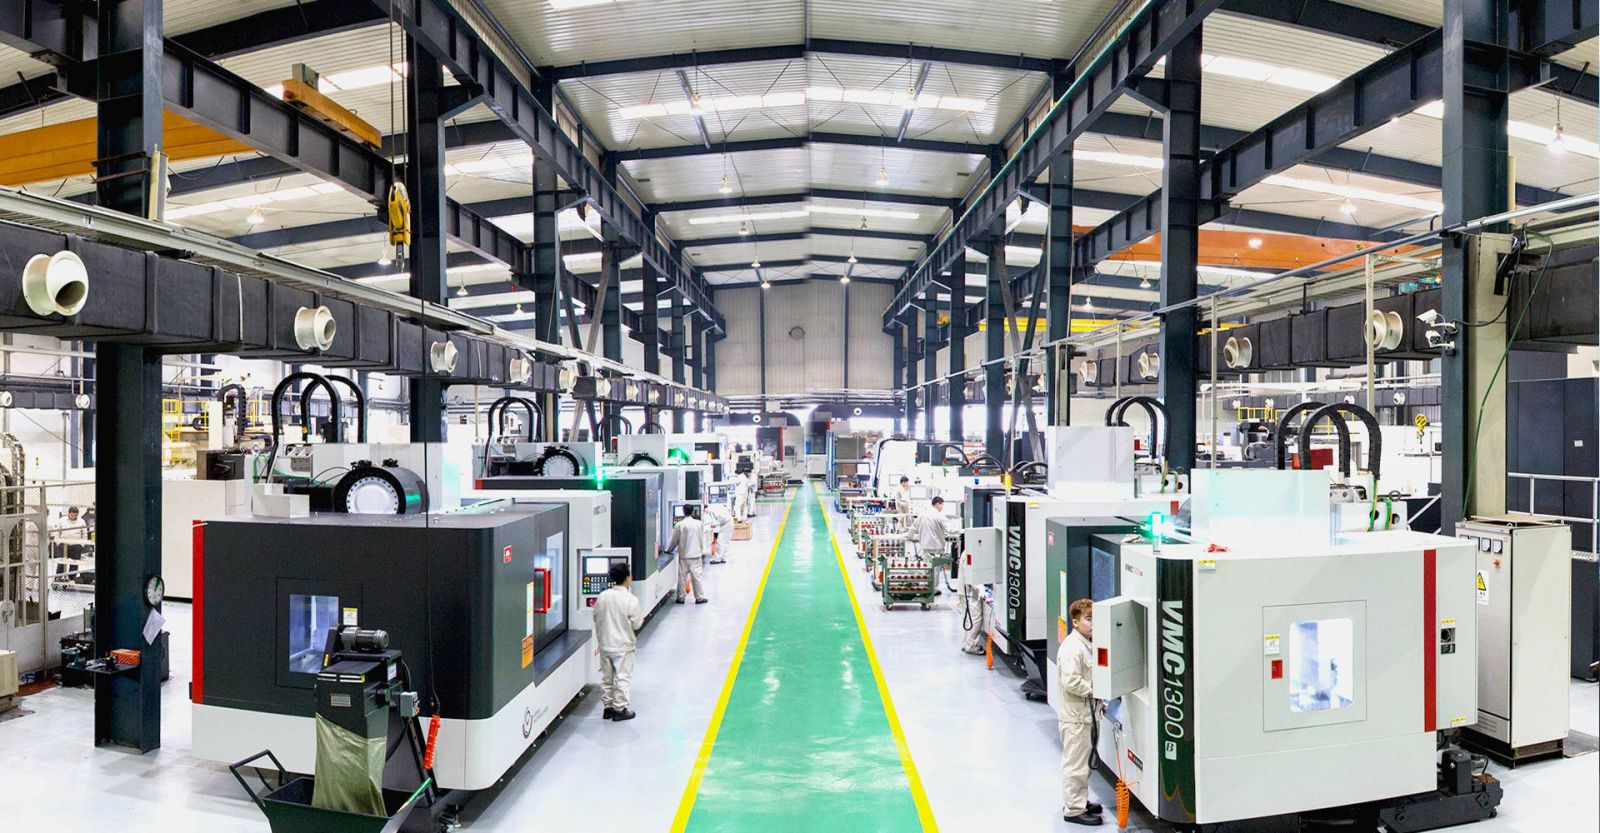
Facility Audit: What to Look For on the Floor
A factory floor tells you more than a capability brochure ever will. Look for:
-
Facility cleanliness and organized workflow
-
Calibration stickers on measurement equipment — are they current?
-
QC area — is it a proper inspection station with environmental controls, or just a desk with a caliper?
-
Non-conformance records — ask to see the log from the past 6 months. How many entries? What corrective actions were taken?
-
Material storage — is raw stock segregated by grade and heat number, or piled in a corner?
-
Work instructions at operator stations — are they posted, current, and in the operator's language?
Key takeaway: Visit the factory or use a third-party inspector. Ask to see non-conformance records — a supplier with zero defects is either lying or not inspecting.
Pillar 6: Cost Evaluation & Negotiation — Beyond the Unit Price
The Total Cost of Ownership Lens
Chasing the lowest unit price is a rookie mistake. The true cost of a sheet metal part includes setup fees, tooling investment, shipping, inventory holding, obsolescence risk, and cash flow impact. A buyer who was quoted three times the expected unit price for a 25-piece order instead of 500 pieces learned this the hard way.
| Cost Factor | High-MOQ Supplier (500+ pcs) | Low-MOQ Supplier (10–50 pcs) |
|---|---|---|
| Unit price | Lower | Higher |
| Inventory holding cost | High | Low |
| Obsolescence risk | High (design changes waste stock) | Low |
| Cash flow impact | Large upfront payment | Smaller, more frequent payments |
| Tooling amortization | Spread across many units | Concentrated on fewer units |
| Scrap/rework exposure | Large batch at risk | Small batch, easier to correct |
For a custom bracket project, a buyer initially wanted 500 pieces to get the best unit price. After a manufacturing cost analysis, ordering in batches of 50 every six weeks cut total cost of ownership by nearly 20% when factoring in warehousing, potential design revisions, and cash flow.
Practical Strategies to Reduce Unit Costs at Low Volumes
-
Provide complete specs early — complete RFQ packages unlock negotiation leverage and can reduce effective costs by 15–30%
-
Negotiate staggered delivery schedules — commit to a total annual quantity but split it into smaller batches with defined delivery dates
-
Offer to pay tooling up front — this makes suppliers more willing to accept low-volume orders
-
Simplify your design — DFM optimization reduces scrap rates and tool wear
DFM Design Optimization for Cost Reduction
Design for Manufacturability (DFM) is the most powerful cost reduction tool available before production begins. Key DFM principles for sheet metal:
-
Bend radii should be equal to or greater than material thickness
-
Formed leg length should be a minimum of 2.5 times material thickness
-
Hole diameter should be equal to or greater than the material thickness being punched
-
Hole placement should be at least 1.5 times material thickness away from bends, edges, and other holes to prevent tearing or deformation
DFM-optimized part designs reduce scrap rates, tool wear, and machine downtime, leading to greater productivity and lower defect rates.
Key takeaway: Calculate total cost of ownership, not unit price. Embed DFM review in your drawing package before quoting.
Pillar 7: Lead Time & Production Capacity Assessment
What Is a Reasonable Lead Time?
A reasonable sheet metal fabrication lead time typically falls between 2 and 8 weeks for custom projects, depending on material availability, part complexity, production volume, post-processing requirements, and supplier coordination.
Evaluating Capacity Utilization
Assess a supplier's capacity utilization rate. The ideal range is 70–85%: high enough to demonstrate operational efficiency, low enough to provide buffer for your orders and expedited requests.
Red flags for capacity:
-
Utilization consistently above 90% — no room for growth or emergencies
-
Inconsistent on-time delivery rates
-
Vague answers about production scheduling systems
Scalability Assessment
Many fabricators excel at one-off work. They have a skilled welder, a single laser cutter, and a small team that gives every part personal attention. But when your order grows from 50 to 5,000 pieces, that same shop hits a ceiling. The welder is overloaded. The laser runs double shifts. Quality slips.
Scalability indicators:
| Factor | Green Flag | Red Flag |
|---|---|---|
| Equipment redundancy | Multiple machines of same type | Single machine for critical processes |
| Capacity utilization | 60–75% with buffer | Over 90% with no room for growth |
| Workforce model | Flexible shifts, cross-trained operators | Fixed single-shift operation only |
| Production planning | Digital scheduling (ERP/MRP) | Manual scheduling on whiteboards |
| Ramp-up track record | Documented 5x scale case study | Vague answers or no examples |
Key takeaway: Start with a pilot project. Place an initial order, track lead time management, first-pass yield, and communication responsiveness before committing to a full-year contract.
Pillar 8: Communication & Cultural Management in Overseas Sourcing
The Hidden Risk That Derails Orders
Technical skill alone does not guarantee success — cultural communication gaps can quietly derail even the most well-planned orders. The gap between what a drawing communicates and what a fabrication shop interprets is the single largest source of quality failures in custom sheet metal sourcing.
Drawing Interpretation Differences
Engineers in different countries are often trained on different standards. Vietnamese engineers, for example, are highly proficient at reading technical drawings but are often trained on JIS or GB standards rather than ASME Y14.5. This means your GD&T symbols may look familiar but carry slightly different interpretation habits.
Practical steps to improve drawing accuracy:
| Step | Action | Why It Works |
|---|---|---|
| 1 | Send 3D STEP files alongside 2D PDFs | Reduces ambiguity on complex bends and cutouts |
| 2 | Highlight critical tolerances in red | Draws immediate attention to must-hold dimensions |
| 3 | Use simple English notes, not paragraphs | Avoids language barriers with technical jargon |
| 4 | Reference ASTM or JIS standards explicitly | Matches terminology engineers already know |
| 5 | Request a marked-up drawing back from supplier | Forces them to confirm their understanding in writing |
| 6 | Include sample photos of acceptable vs. rejected parts | Visual references cut through any language gap |
The "Yes" Trap and Face-Saving Culture
In many Asian business cultures, a supplier may say "yes" to show respect, even when they do not fully understand a requirement. This is not dishonesty — it is rooted in business culture where avoiding "loss of face" is important.
Solution: Do not rely on verbal confirmation. Require written confirmation of every specification through a structured DFM review. Run a mandatory "drawing review meeting" before any project enters production. Go through every tolerance, every surface finish callout, and every critical feature. Ask the supplier to mark up the drawing with their understanding. This simple step has eliminated most first-article failures.
Structured Feedback Loops
Establish a closed-loop quality feedback system that connects defect detection directly to process control. This includes drawing reviews, in-process inspections, pre-shipment verification, and structured corrective actions.
Key takeaway: Use visual communication, require written confirmation, and build a structured DFM review into every project. Never assume a "yes" means understanding.
Pillar 9: Quality Issue Resolution & Risk Management
Non-Conformance Handling: The 8D Process
When a quality issue occurs, the supplier's response reveals their true quality culture. Require suppliers to follow the 8D problem-solving methodology:
| Step | Action | Timeline |
|---|---|---|
| D1 | Establish a team | Within 24 hours |
| D2 | Define the problem | Within 24 hours |
| D3 | Containment action (100% inspection of suspect batches) | Within 24–48 hours |
| D4 | Root cause analysis | Within 7 days |
| D5 | Corrective action selection | Within 14 days |
| D6 | Implementation and validation | Within 30 days |
| D7 | Preventive action (systemic change) | Within 60 days |
| D8 | Team recognition and closure | Upon verification |
If defective material is found, your recourses usually include scrap, rework or repair, use "as is," or return to the supplier for replacement.
Building a Closed-Loop Quality Feedback System
A closed-loop system integrates drawing reviews, in-process inspections, pre-shipment verification, and structured corrective actions to prevent recurring defects and achieve right-first-time results. The key is connecting defect detection directly to process control — enabling real-time corrections during cutting, bending, and welding.
Payment Terms & Financial Risk Mitigation
Metal fabrication payment cycles span 60–90 days, and steel and aluminum price volatility compounds payment delay risk. Best practices for payment risk management include:
-
Tie payment milestones to production stages, not calendar dates
-
Require a formal contract specifying prepayment ratio, product specifications, delivery terms, and quality inspection standards
-
Use inspection-linked payment terms — final payment released only after incoming inspection passes
-
Consider non-recourse financing to protect against buyer non-payment risk on approved invoices
Tariff & Trade Risk Management
Section 232 tariffs on steel and aluminum products can reach up to 50% in some cases. Moving sheet metal sourcing from China to Vietnam can reduce total duties from over 300% to approximately 70%.
Mitigation strategies:
-
Verify HTS codes for every part classification
-
Factor tariff exposure into total landed cost calculations
-
Diversify across multiple countries to reduce single-country tariff risk
-
Monitor policy changes — spot prices on hot-rolled steel coil and aluminum sheet can swing significantly during periods of policy uncertainty
Key takeaway: Require 8D corrective action reports for every quality escape. Tie payment to production milestones. Model tariff exposure into your landed cost.
Pillar 10: New Product Introduction (NPI) & Prototype-to-Production Transition
Why the Prototype-to-Production Transition Fails
The transition from prototype to mass production is where quality systems are truly tested. Many suppliers who deliver excellent prototypes cannot sustain that quality at volume. Prototypes built with production-intent material and routing reveal issues like springback and weld distortion while corrections remain fast and low cost.
The NPI Process Framework
| Phase | Sheet Metal Considerations | Key Deliverables |
|---|---|---|
| Feasibility & DFM | Bend relief geometry, grain direction, weld access clearance | DFM report, MBOM, material selection |
| Prototyping (EVT/DVT) | Production-intent routing (CNC press brake, robotic cells) | Functional prototypes, dimensional check |
| Pilot & Process Validation (PVT) | Hardware insertion verification, fixture validation, tolerance stack-up | FAI per AS9102, PFMEA, control plan, CPK studies |
| Production Launch | SPC on critical features, process capability monitoring | PPAP package, work instructions, corrective action records |
Early DFM collaboration delivers the strongest impact, because it catches design issues like bend relief, weld access, and tolerance stack-ups while changes remain inexpensive.
Prototype-to-Production Transition Strategies
Bridge Production is a transitional manufacturing phase between prototyping and production. It enables you to produce low-volume runs of a product that can be sold or used while the permanent, high-volume manufacturing process is being set up.
Tooling transition trigger points: Typically, transitioning from soft tooling to hard tooling becomes economically viable at several thousand to tens of thousands of annual units. This balances cost, quality consistency, and lead-time risk.
Key takeaway: Require a formal NPI process with DFM review, EVT/DVT prototyping, PVT validation, and PPAP documentation. Start with a pilot project before committing to full production.
Summary Checklist: The Overseas Sheet Metal Supplier Audit Card
| QC Metric | What to Ask / Request | Verification Method |
|---|---|---|
| QMS Certification | ISO 9001:2015 Certificate | Check certificate validity and scope with issuing body |
| Industry Certifications | IATF 16949 / ISO 13485 / AS9100D | Verify against registrar accreditation records |
| Raw Material | Material Test Certificate (MTC) per EN 10204 3.1 | Compare heat number on steel with certificate |
| Material Traceability | Heat number tracking from receiving to finished parts | Request lot traceability records for a recent order |
| First Article | FAI Report + Golden Sample | Review dimensional accuracy before mass run |
| Precision Measurement | CMM Inspection Report | Mandatory for tight-tolerance features |
| Coating/Finish | Salt Spray (ISO 9227) & Film Thickness Report | Verify corrosion resistance compliance |
| In-Process QC | First-off inspection records, AQL sampling data | Review IPQC logs from a recent production run |
| Equipment Calibration | Calibration certificates traceable to NIST | Check calibration stickers during site audit |
| Outgoing QC | Final dimensional inspection report | Require numerical measured values, not "OK" stamps |
| MOQ & Cost | Total cost of ownership calculation | Compare unit price + setup + tooling + inventory + shipping |
| Lead Time | Historical on-time delivery rates | Assess capacity utilization (70–85% ideal) |
| Scalability | Equipment redundancy, ramp-up case studies | Verify multiple machines for critical processes |
| Communication | Structured DFM review process | Require marked-up drawing confirmation |
| Quality Issues | 8D corrective action reports | Review NCR logs from past 6 months |
| Payment Terms | Milestone-based payment schedule | Tie payments to inspection-linked milestones |
| NPI Process | DFM review, FAI, PFMEA, PPAP package | Verify phase-gate deliverables |
| Tariff Exposure | HTS code classification | Model landed cost with tariff scenarios |
Five verbal questions worth asking during any factory visit:
-
Which operations are done in this building, and which are subcontracted?
-
What happens to a part that fails inspection — rework, scrap, or concession?
-
How is a repeat order set up, and what does the operator work from?
-
What is outside your capability, and who do you refer that work to?
-
Can you show me your non-conformance log from the past 6 months?
The answers to these five questions describe an operation more accurately than a gallery of machinery.
Call to Action
Looking for a Verified Sheet Metal Partner with Strict Quality Control?
quality is built into every step of our manufacturing process. From ISO 9001 certification and CMM inspection to full MTC material traceability, we guarantee zero-defect sheet metal parts for your global orders. We welcome factory audits, third-party inspections, and sample orders — because we believe that verified quality is the foundation of every successful supply chain partnership.
What we offer:
-
ISO 9001:2015 certified quality management system
-
Full material traceability with EN 10204 3.1 MTC on every batch
-
CMM inspection reports for tight-tolerance features
-
First Article Inspection with golden sample retention
-
ISO 9227 salt spray testing for all coated products
-
8D corrective action process for every quality escape
-
Complete factory audit packets available on request
-
NPI support from prototype through production launch
Send us your CAD drawings today to request a sample or a complete factory audit packet. Let us prove that overseas manufacturing doesn't have to mean quality compromise.
[Request a Sample / Upload RFQ with QC Requirements]
Have a question about evaluating a specific QC capability? Our engineering team is available to walk you through our quality documentation, inspection records, and certification details. Contact us at [email/phone] or submit your RFQ through our online portal.
Get Your Custom Quote Today
- Contact Us: Share your project details with our experienced team, and let us provide tailored solutions for your unique needs.
- Fast & Competitive Pricing: Receive a detailed quote quickly, ensuring your project stays on track.
- Reach Out Anytime:
- Email: [email protected]
- Call/WhatsApp: +86 13355741031
- Live Chat: Connect with our support team instantly via our website's chat feature